Component-level support for tank-floor corrosion screening scanners — permanent magnets, flux-return steel, sensor mounting and rugged mechanical structures designed around your scanner.
Tank-floor MFL combines a magnetic circuit with a moving mechanical platform. Plate condition, debris, coatings and scanning motion all influence the sensor environment.
Plate thickness and material, pole geometry and the magnetic return path determine whether the circuit can support useful metal-loss screening.
Coatings, weld profiles, plate steps, debris and scanner motion can change the sensor-to-plate gap. Mechanical guidance and wear parts matter.
MFL is a screening method. Top-side versus bottom-side discrimination and remaining-thickness sizing may require complementary sensing or ultrasonic verification.
The magnetic bridge attracts ferrous debris and the scanner sees repeated impact. Retention, cleaning access and replaceable protection must be engineered in.
The scanner magnetizes a local region of carbon-steel floor plate and reads disturbances in the flux as it travels. The diagram is schematic and not to scale.
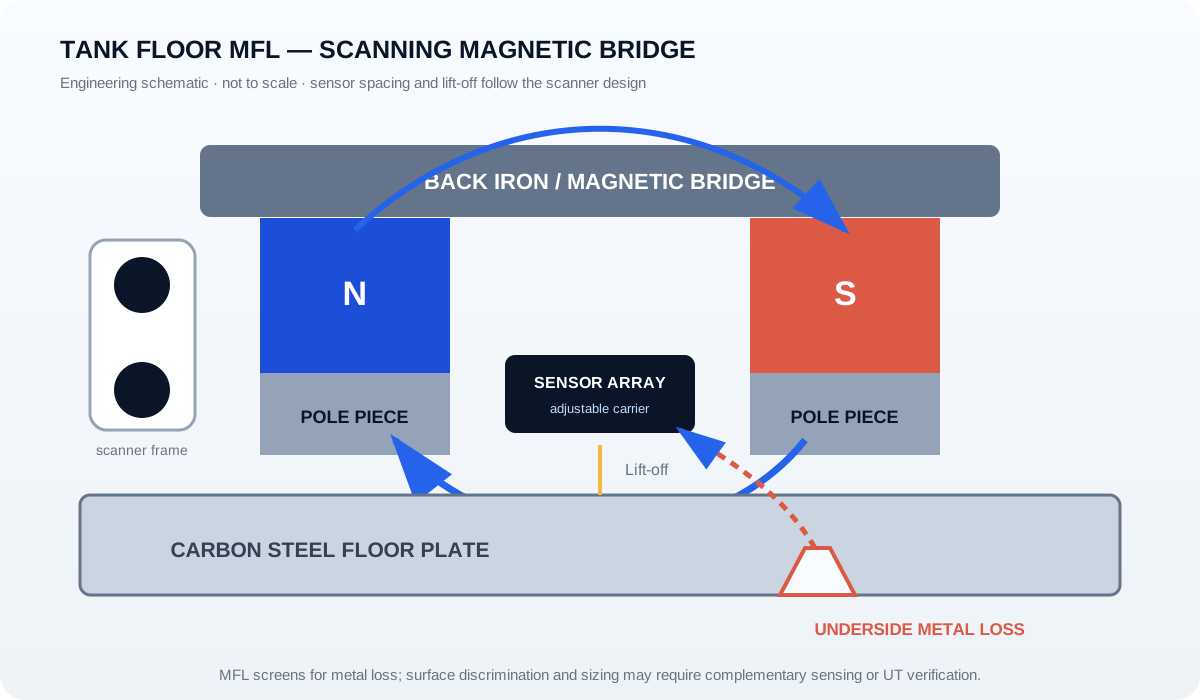
We support the magnetic bridge and its surrounding mechanical structure, with the supply scope split according to your drawings and assembly strategy.
NdFeB blocks or custom profiles supplied with defined grade, coating, polarity, magnetization direction and batch traceability.
Steel return-path components and integrated bridge arrangements matched to the scanner’s pole spacing and available envelope.
Machined pole components that shape the working region and interface with the plate-side wear system.
Brackets, carriers and adjustment features for customer-specified Hall or coil sensor layouts and lift-off targets.
Supports, cross-members, spacers, handles, fixing details and retention structures supplied to the agreed mechanical scope.
Replaceable contact parts and non-magnetic protective elements where required, designed to support cleaning and maintenance.
A useful component discussion must respect the limits of the inspection method as well as its strengths.
| Question | Engineering interpretation | Design / procedure implication |
|---|---|---|
| Can MFL screen for corrosion-related metal loss? | Yes, it is widely used to screen carbon-steel tank floors for local magnetic-flux disturbances associated with metal loss. | Calibration, scan coverage and signal processing remain system-level responsibilities. |
| Can basic MFL always separate top-side from bottom-side corrosion? | No. Surface discrimination is not guaranteed by the magnetic bridge alone. | Use complementary sensing and/or verification methods defined by the inspection procedure. |
| Does an MFL indication directly equal remaining thickness? | Not without calibration and sizing procedures. Signal response depends on geometry, lift-off, material and defect form. | Confirm selected indications with UT or another specified method where required. |
Scanner specifications and acceptance criteria must come from the equipment designer and the applicable inspection procedure, not from a generic component page.
Drawings and operating conditions let us discuss the magnetic circuit and mechanical structure together. If some items are unknown, mark them as open rather than guessing.
No inspection service is implied by this page. XAK supports magnetic and mechanical components for companies developing or manufacturing scanning equipment.
Yes. The package can include magnets, back iron, pole pieces, sensor carriers, structural brackets, fixing details and wear-related parts according to the agreed drawing.
Basic MFL should not be assumed to provide reliable surface discrimination by itself. The inspection system may need complementary sensing and UT or other verification.
Wear changes pole contact, working gaps and sensor lift-off. Those changes can affect the signal just as directly as a change in magnet grade.
Send your drawing, application conditions and target integration level. XAK will respond within 24 hours.
Contact →Request a Quote